Sheet Metal Fabrication Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery
CNC Machining Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery
Plastic Injection Molding Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery
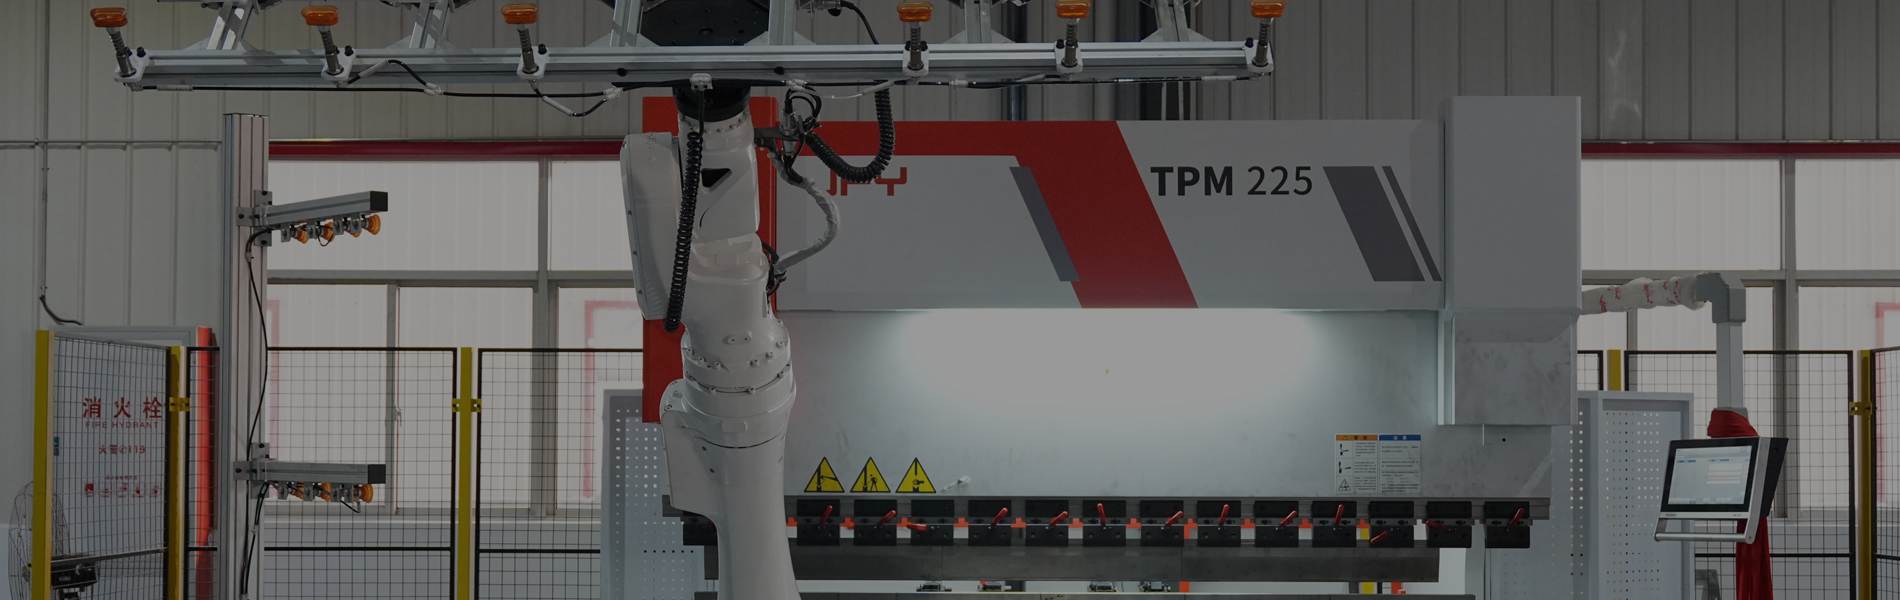
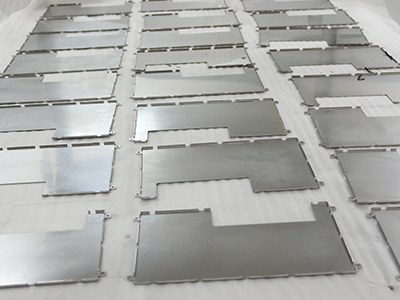
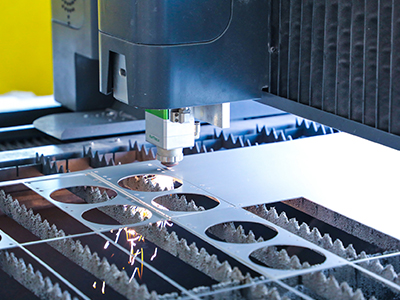
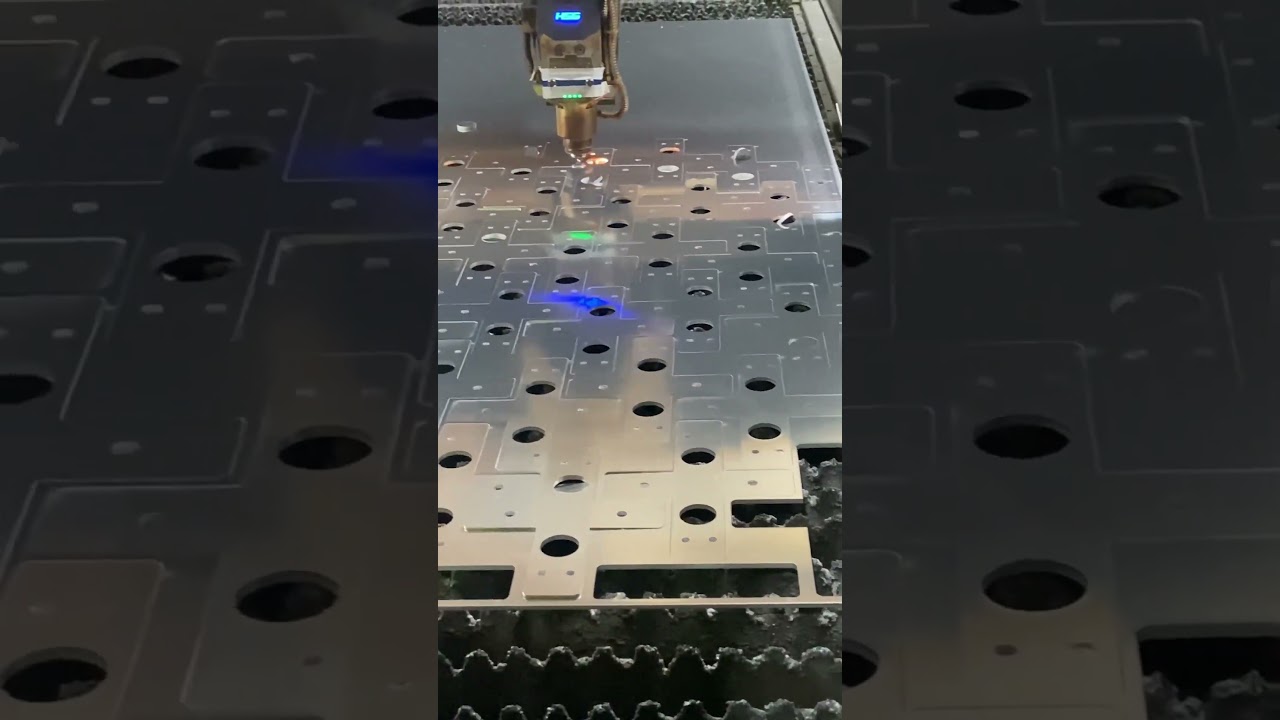
Custom laser cut sheet metal parts in steel, stainless steel, aluminum and brass, prepared for bending, welding and assembly.
✓ Multi-process fabrication under one project ✓ Engineering review before production ✓ Prototype-to-production support

Share your drawing, material and quantity for engineering review.
| Material | Grades We Can Review | Cutting Thickness* | What It Means for Your Project |
|---|---|---|---|
| Carbon Steel | Q235, Q345, SPCC, SPHC | Up to 25 mm | Suitable for brackets, panels and structural parts. Specify corrosion protection and any subsequent welding or coating. Oxygen-cut edges may require oxide removal before powder coating or painting. |
| Stainless Steel | SS201, SS304, SS316, SS430 | Up to 16 mm | For stainless steel laser cutting, select the grade around the service environment, appearance and joining requirements. Identify visible surfaces and specify any brushing, polishing or passivation needed after fabrication. |
| Aluminum | 5052, 5083, 5754, 6061 | Up to 12 mm | For aluminum laser cutting, review the alloy and temper together with any subsequent bending. For parts with cosmetic surfaces, specify which faces require protection and the intended finish. |
| Brass & Copper | H62/H65 brass; copper grades reviewed individually | Reviewed by grade and drawing | Send the exact material designation, thickness and intended use. Cutting feasibility, edge requirements and any subsequent forming or finishing are reviewed for the project. |
| Comparison Factor | Laser Cutting (Fiber) | Wire EDM |
|---|---|---|
| Process Mechanism | Thermal cutting via focused laser beam. | Electrical discharge erosion via thin charged wire (no contact). |
| Typical Tolerance | ±0.05 – ±0.1 mm | ±0.005 – ±0.02 mm |
| Material Thickness | Thin–medium sheets (0.5–25 mm). | Thick / hard blocks (up to ~300 mm). |
| Cost | Lower per part (sheet production). | Higher per part (slow process). |
| Geometry Capability | Complex 2D profiles, intricate patterns. | Complex 2D profiles in thick / hard materials. |
| Edge Quality | Smooth, minimal burr; small HAZ. | Excellent edge quality, no thermal stress. |
| Heat-Affected Zone (HAZ) | Small but present. | Effectively none (cold process). |
| Production Speed | Very fast for sheet metal nesting. | Slow (mm/min range). |
| Material Waste | Low (CAM nesting). | Minimal (kerf only). |
| Typical Materials | Carbon steel, stainless, aluminum, brass, copper. | Any conductive material — hardened tool steel, carbide, Inconel, titanium. |
| Ideal Use Case | Sheet metal panels, enclosures, structural parts. | Tool & die, precision punches/dies, turbine slots. |
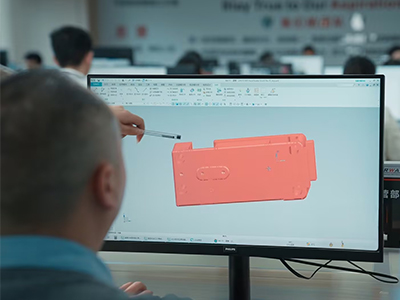
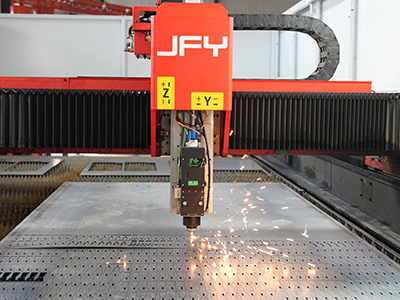
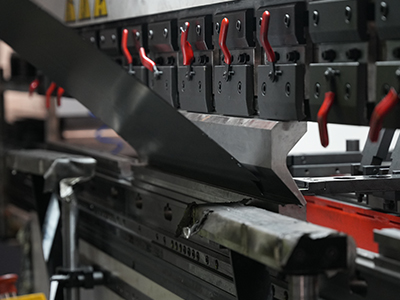
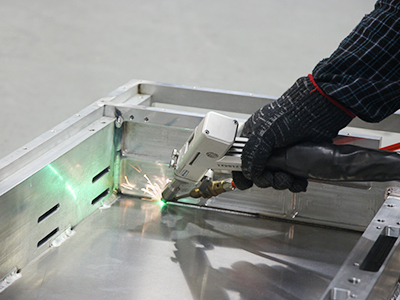
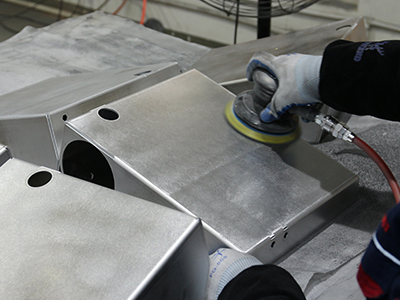
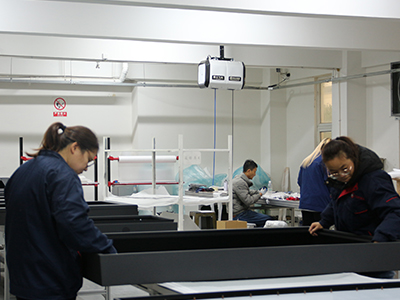
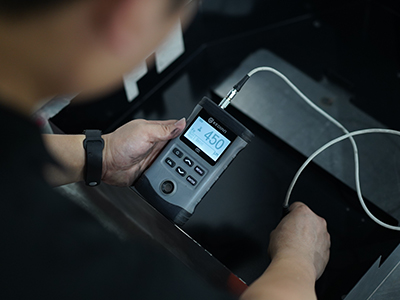
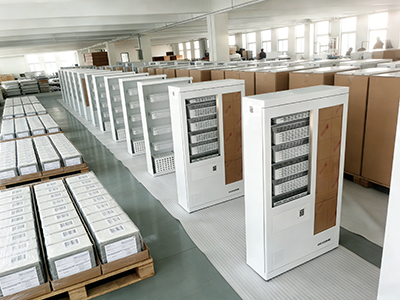
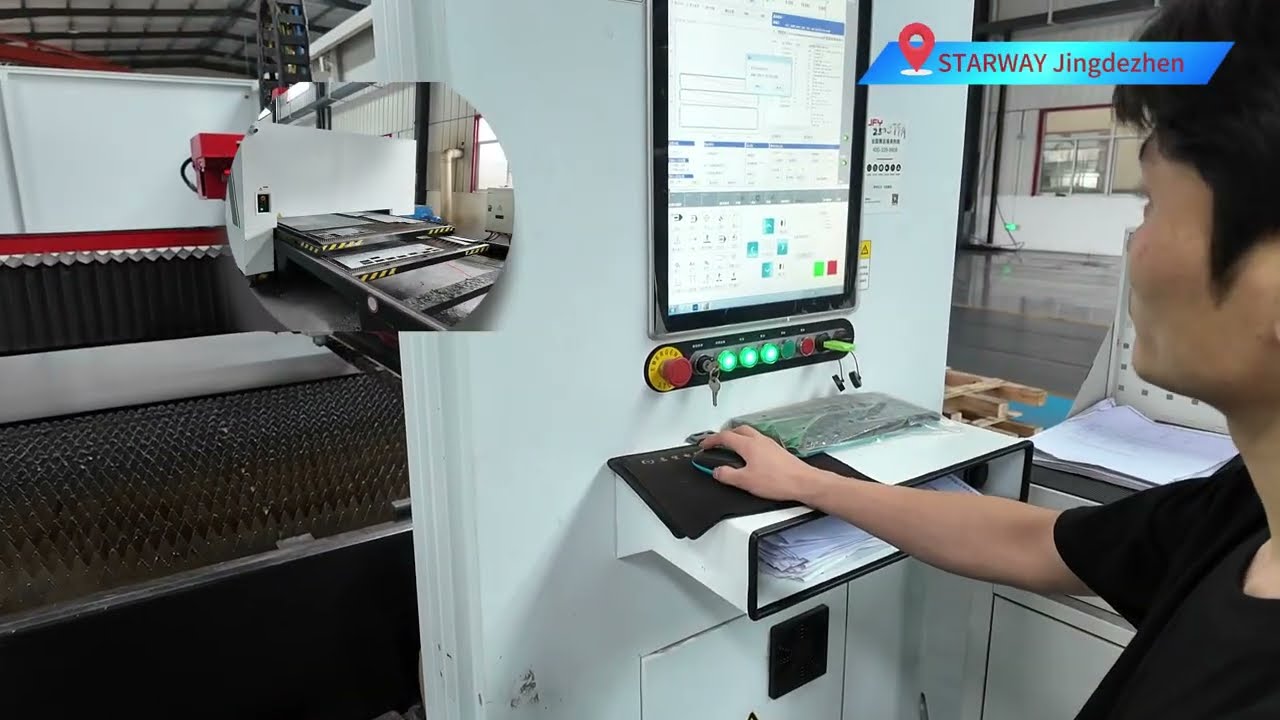
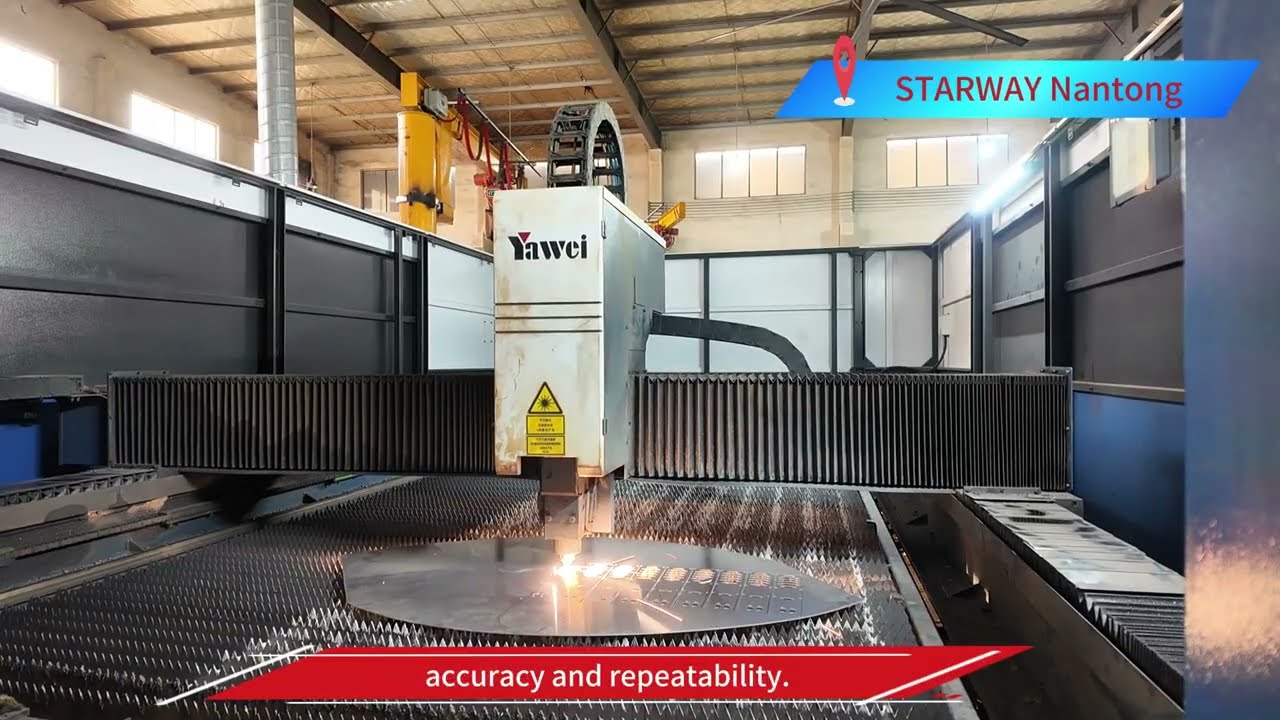
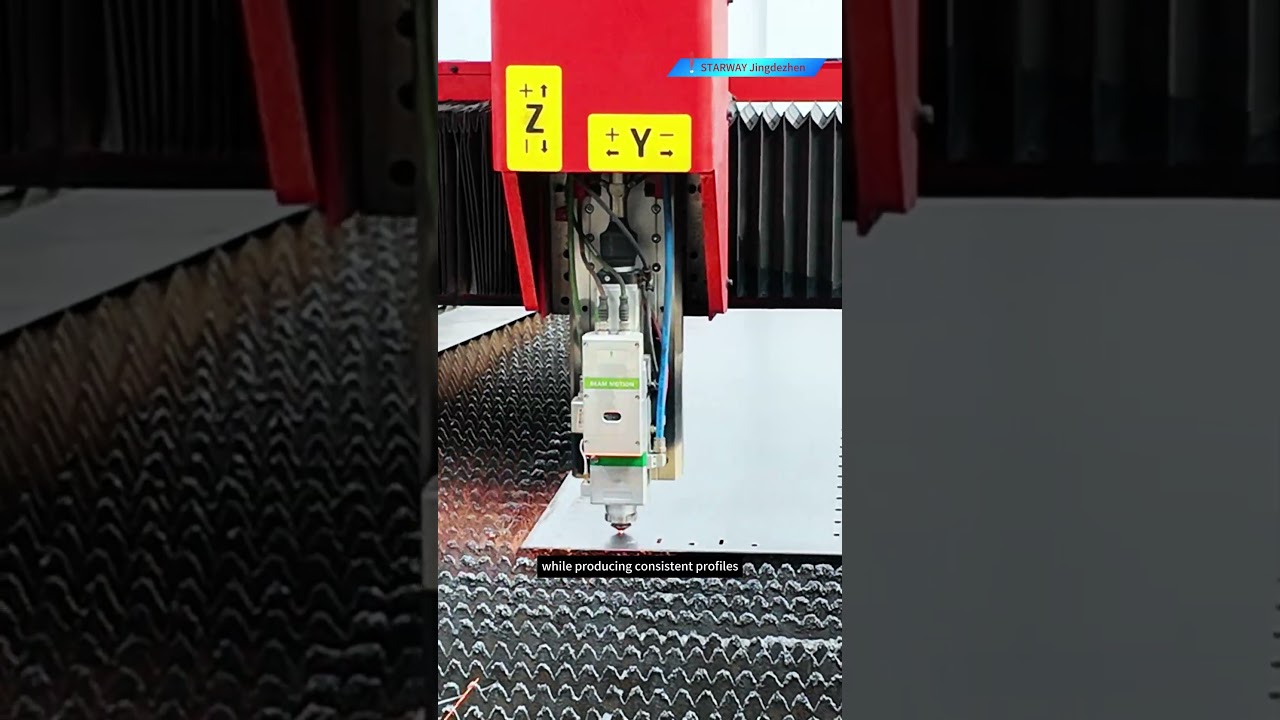
STARWAY’s metal laser cutting services cover carbon steel, stainless steel, aluminum, brass and copper. The applicable thickness depends on the grade, part geometry and edge requirements, as well as the equipment selected for the job. Include the exact material designation and thickness in your drawing. Any proposed material or thickness substitution requires your approval.
The standard cutting tolerance is ±0.1 mm for sheet up to 3 mm thick. For plate over 3 mm, allow ±0.2 mm or more, with the applicable tolerance confirmed during engineering review. Mark critical holes and mating features on the drawing. Tight fitting holes may require drilling or reaming after cutting rather than relying on laser cutting alone.
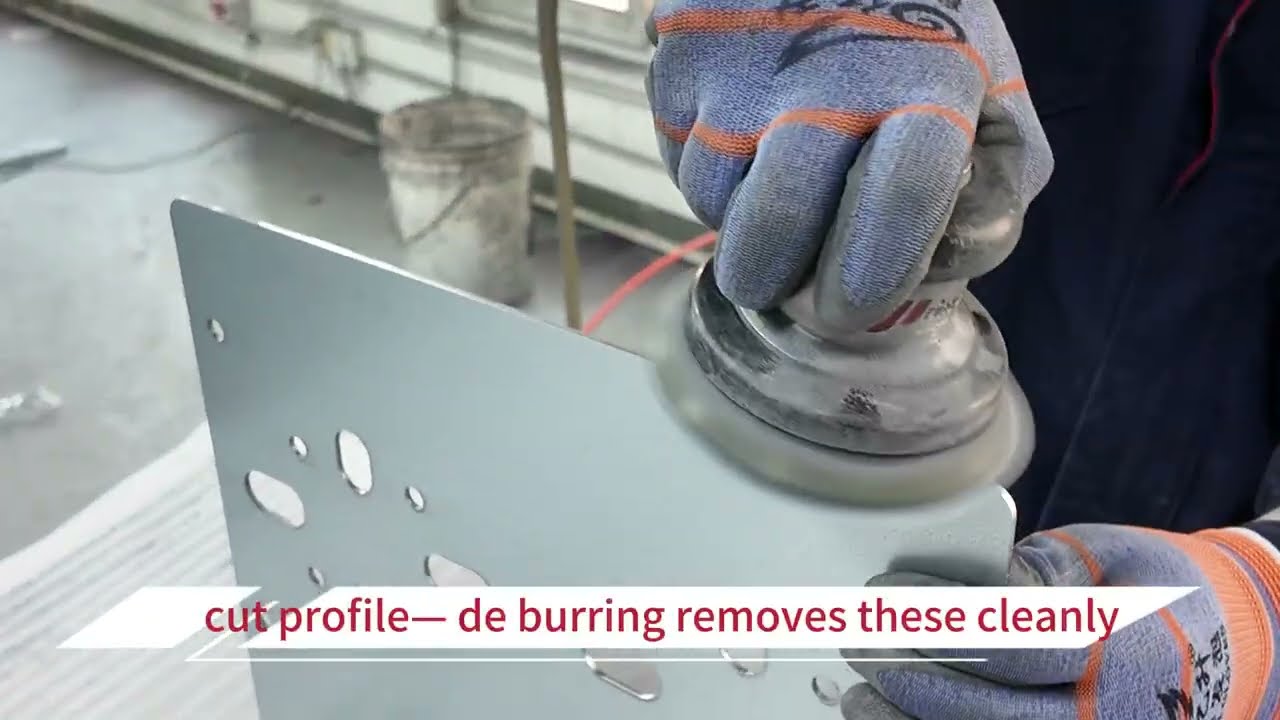
Deburring and edge preparation depend on the material, thickness, cutting conditions and intended use. Specify whether edges will be handled, welded, coated or visible in the finished assembly. Oxygen cut carbon steel edges may need oxide removal before coating. STARWAY reviews these requirements with the cutting route; laser cutting should not be treated as a guarantee of burr free or coating ready edges.
Material grade, thickness, quantity, profile complexity, small holes and narrow gaps all affect the manufacturing review. Identify critical hole sizes, hole to edge distances and any features that must fit other components. STARWAY can review whether features should be laser cut or completed by secondary machining. Include subsequent bending and welding so the quote covers the complete part requirements.
Send DXF or DWG profiles for flat parts, together with a PDF drawing showing dimensions, tolerances and revision. STEP or IGES models can support review of formed parts or assemblies. Include material grade, thickness, quantity, finish and target delivery date, plus any bending or welding requirements. File size: < 130 MB. STARWAY reviews the information before confirming the quotation and manufacturing route.
Yes. STARWAY supports prototype and production projects, with prototype lead time typically 1–2 weeks depending on process and complexity. Material availability, secondary operations, finishing, inspection and quantity affect the schedule. Share the drawing revision and target date so the project team can review feasibility and confirm timing. Repeat orders should reference the approved drawing and agreed acceptance requirements.
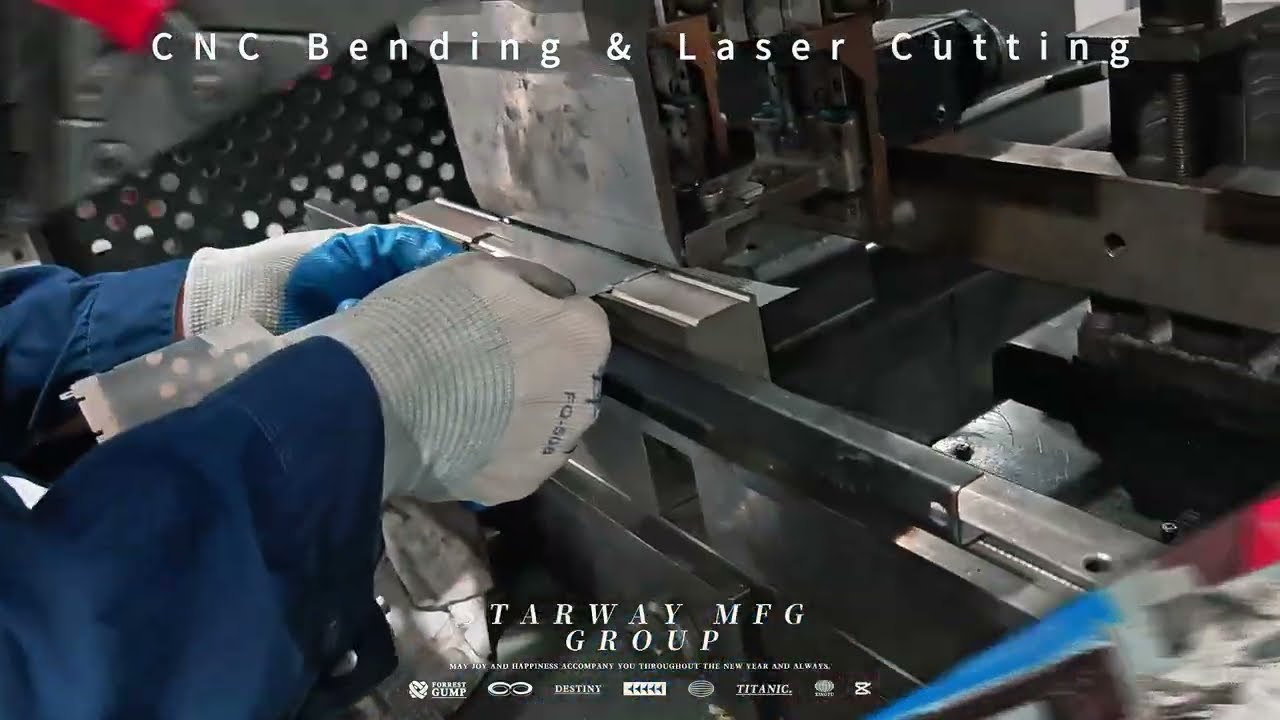
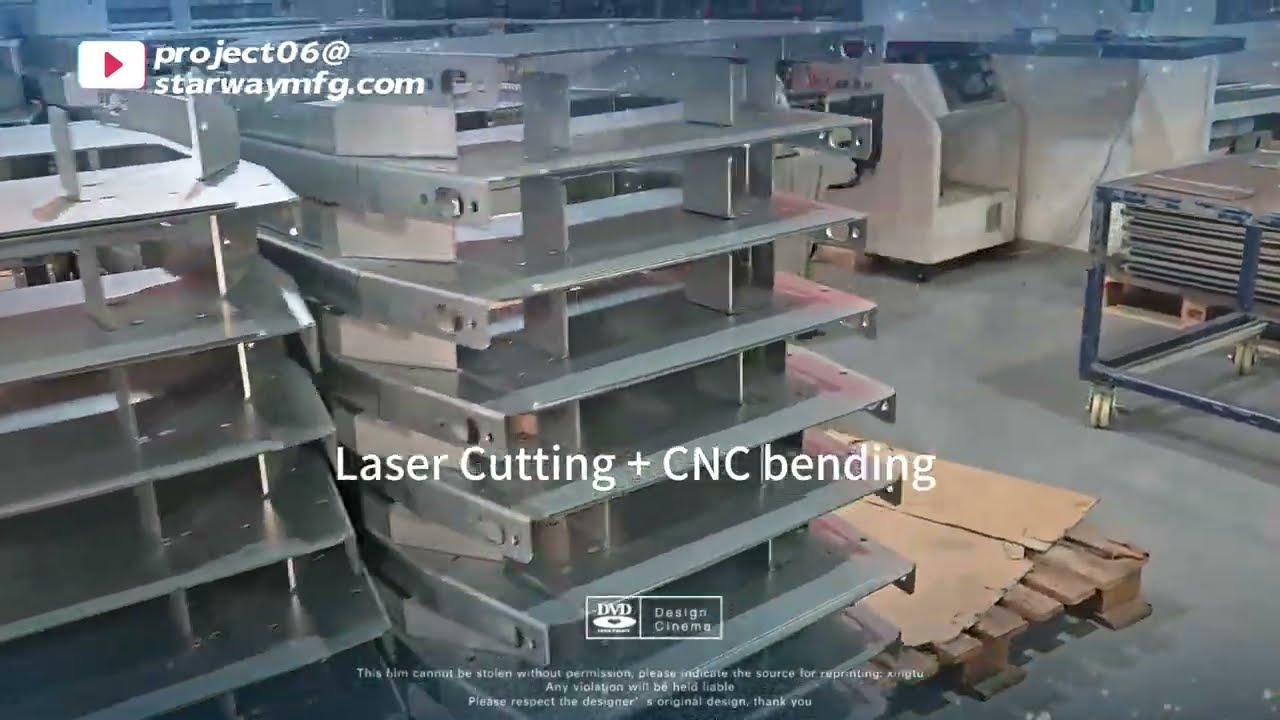
Yes. A project can combine flat sheet laser cutting with CNC bending, welding, grinding, surface finishing, hardware insertion and assembly, as required by the drawing. STARWAY reviews the operations together to address interfaces, edge preparation and finish requirements. Round, square and rectangular tube projects are reviewed separately through our Tube Laser Cutting service; flat sheet capability limits should not be applied to tubes.
STARWAY uses first article inspection, in process checks and final inspection to verify agreed requirements. For laser cut parts, the plan can cover the outer profile, critical dimensions, hole sizes and locations, edge condition and visible surfaces. If the project includes subsequent fabrication, assembly fit and finish requirements are also reviewed. Inspection reports are available on request; confirm the required records before production.

This website uses cookies to provide you with a personalized browsing experience and analyze website traffic. By clicking "Accept", you agree to our use of cookies.
 Global