Sheet Metal Fabrication Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery
CNC Machining Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery
Plastic Injection Molding Design Engineering Project management Assembly Rapid Prototyping Packaging Shipping & Delivery

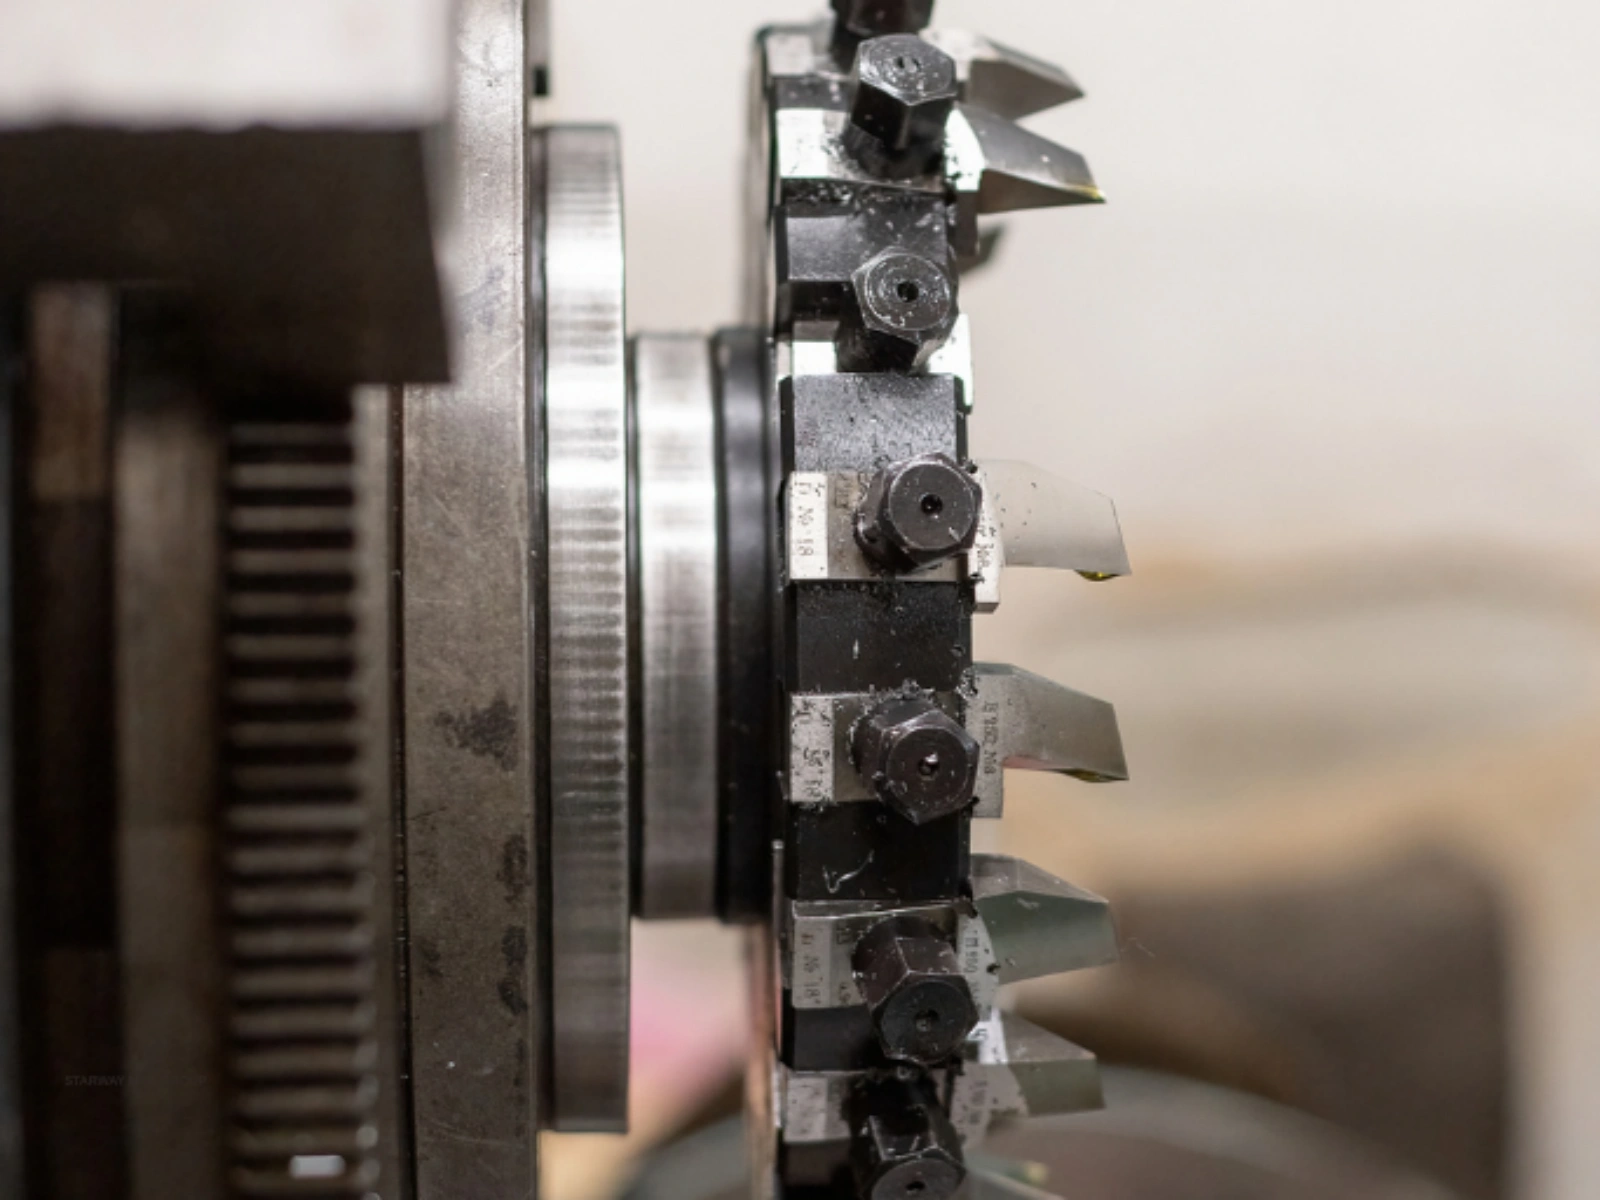
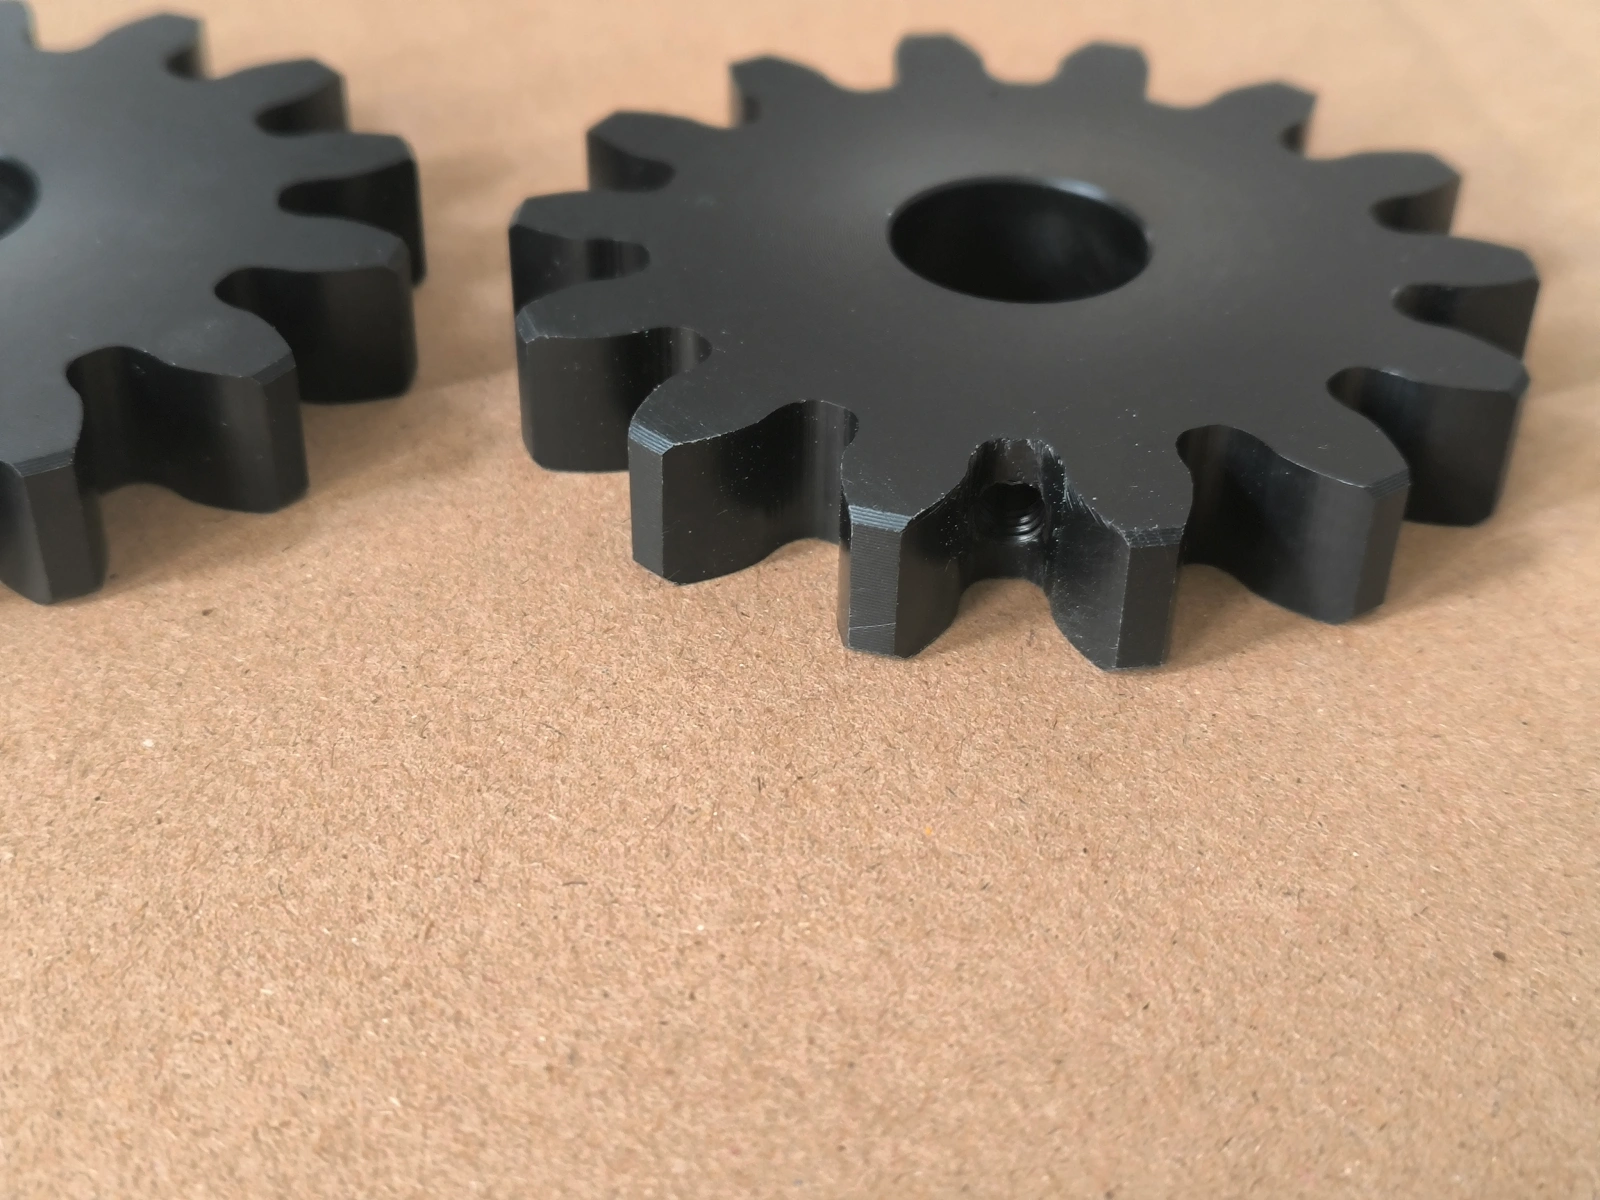
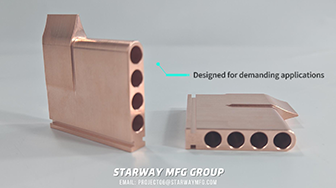
Wire EDM, gear hobbing, drilling and tapping for features that need a dedicated process beyond standard milling or turning.
✓ Processes reviewed around the required features ✓ Material, tooling and access considered together ✓ Inspection requirements defined before production

Start with the feature that needs a dedicated cutting method and the drawing information that defines it.
Material / Thickness / Profile / Tolerances
Gear Type / Module / Tooth Count / Drawing
Finished Diameter / Depth / Position / Datums
Thread Standard / Size / Pitch / Usable Depth
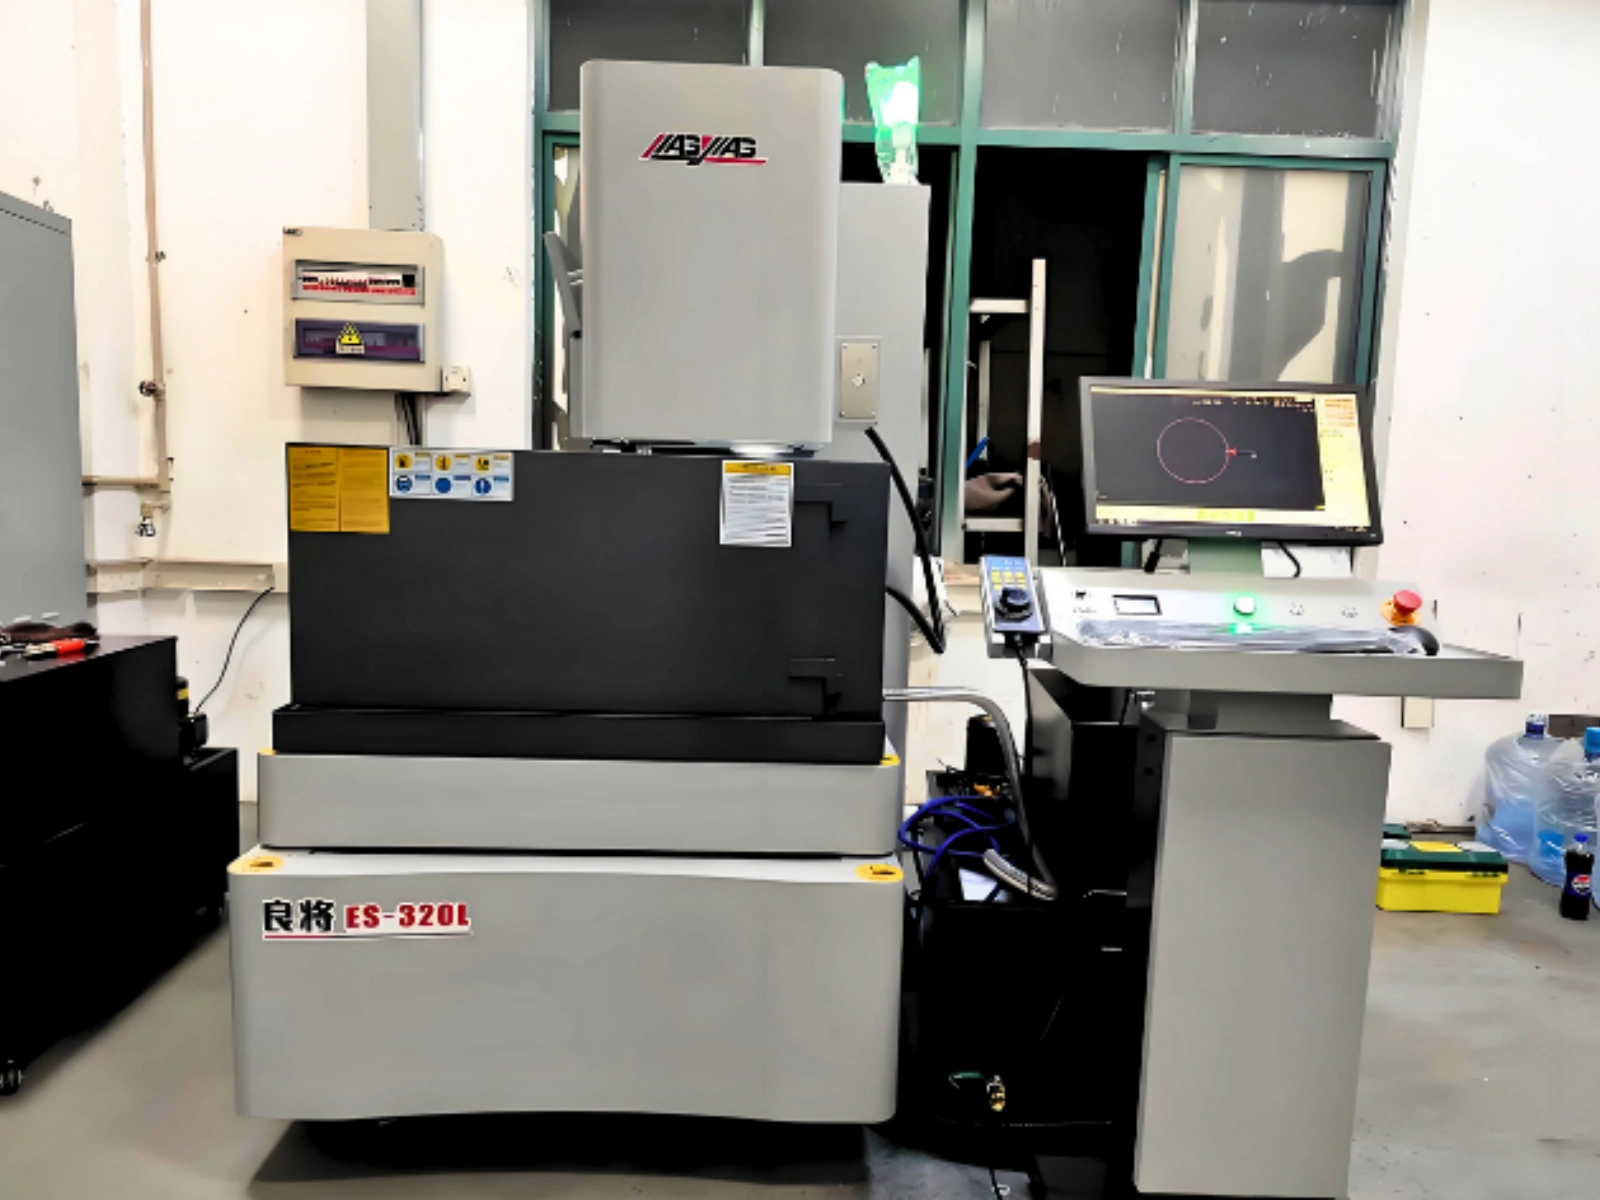
Wire EDM services can be reviewed for through-profiles in electrically conductive materials, including features where conventional cutting-tool access is restricted.
EDM wire cutting produces through-cuts along the wire path, not blind pockets. Feasibility is confirmed for your drawing and available equipment
Internal gears and shoulder-restricted features may require a different process, such as gear shaping. They are not automatically included in the hobbing scope.
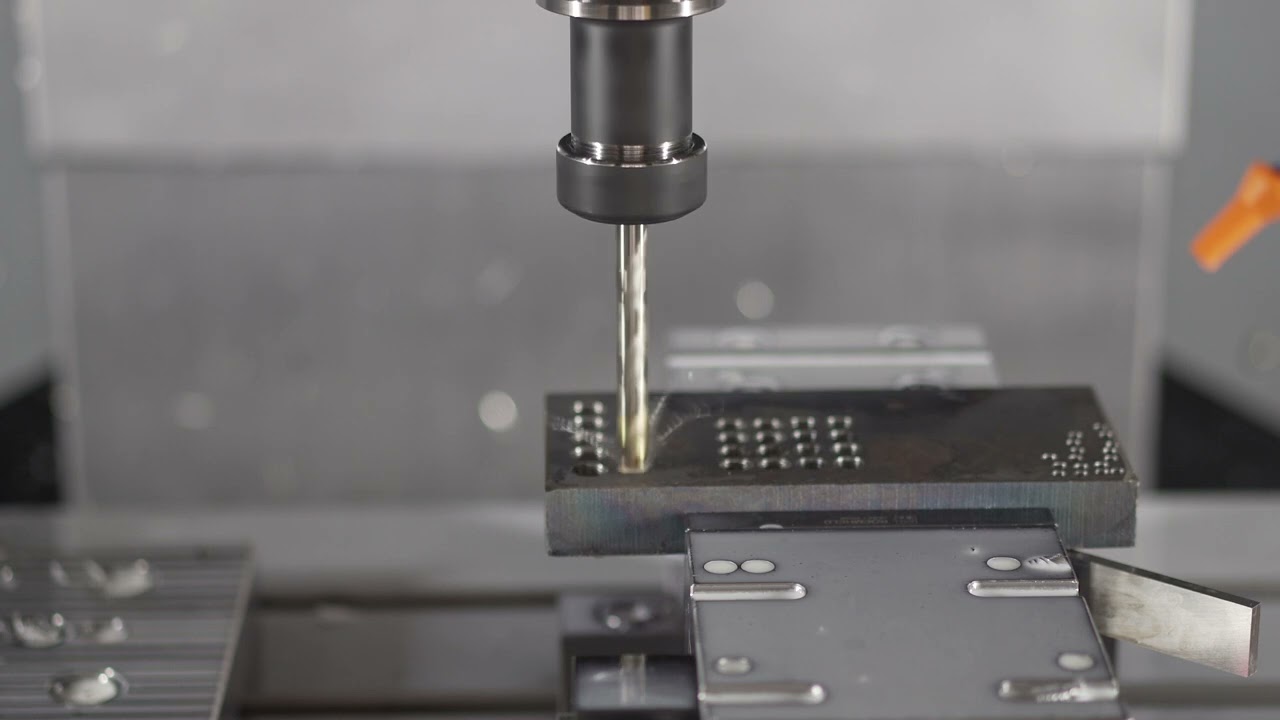
Specify drilling and tapping services around the finished feature, its datums and mating components.
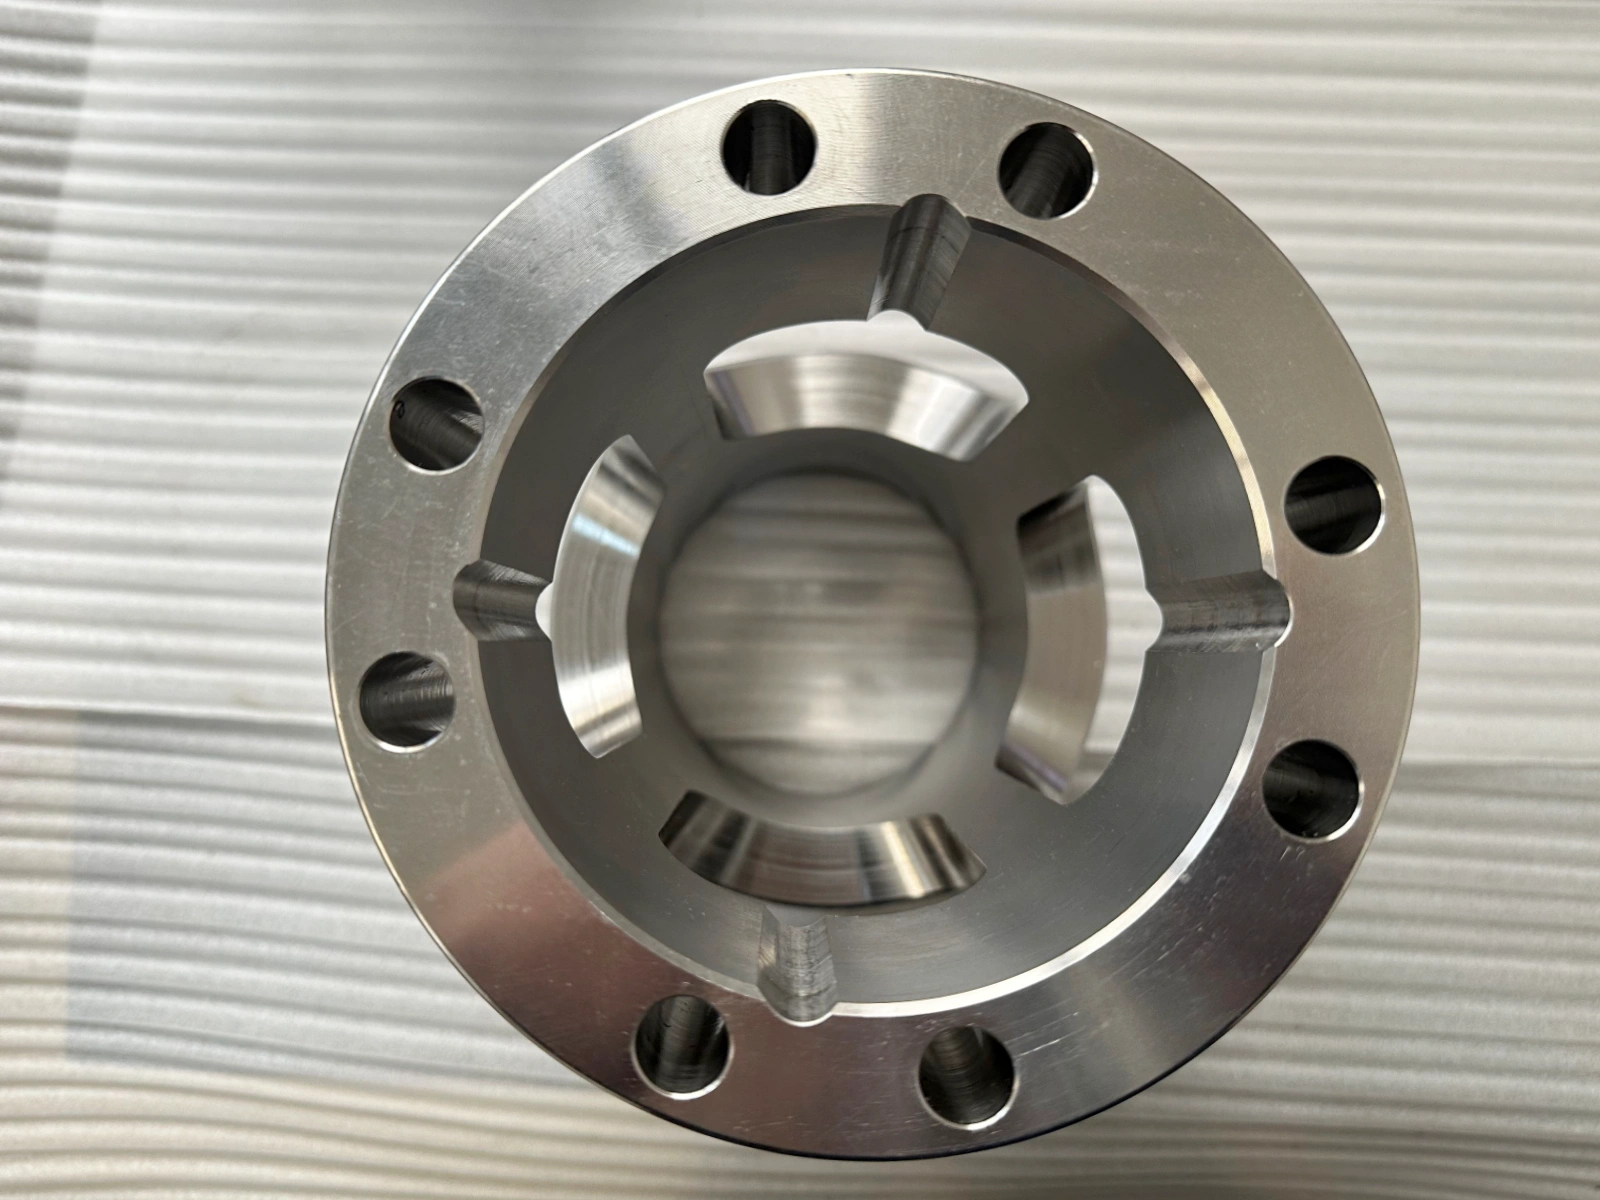
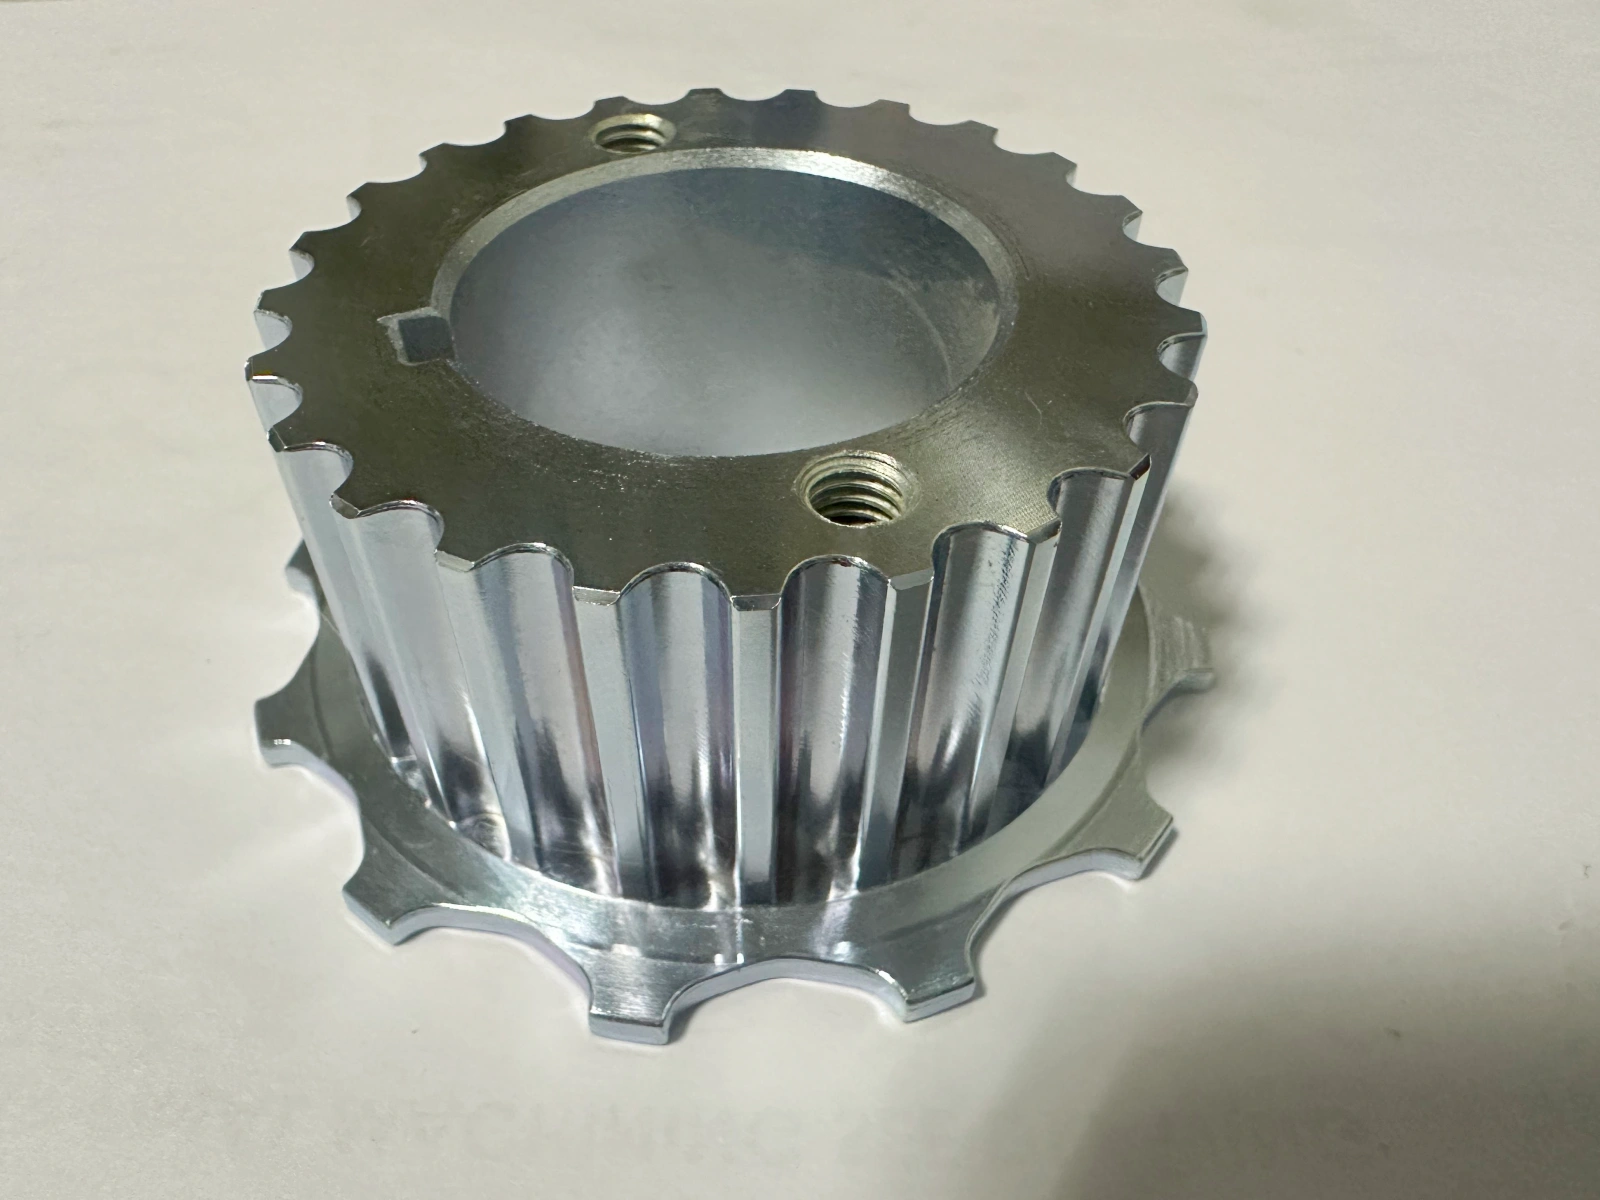
Reaming, boring or another finishing operation may be needed for particular hole requirements. The route is reviewed rather than assumed from the feature name alone.
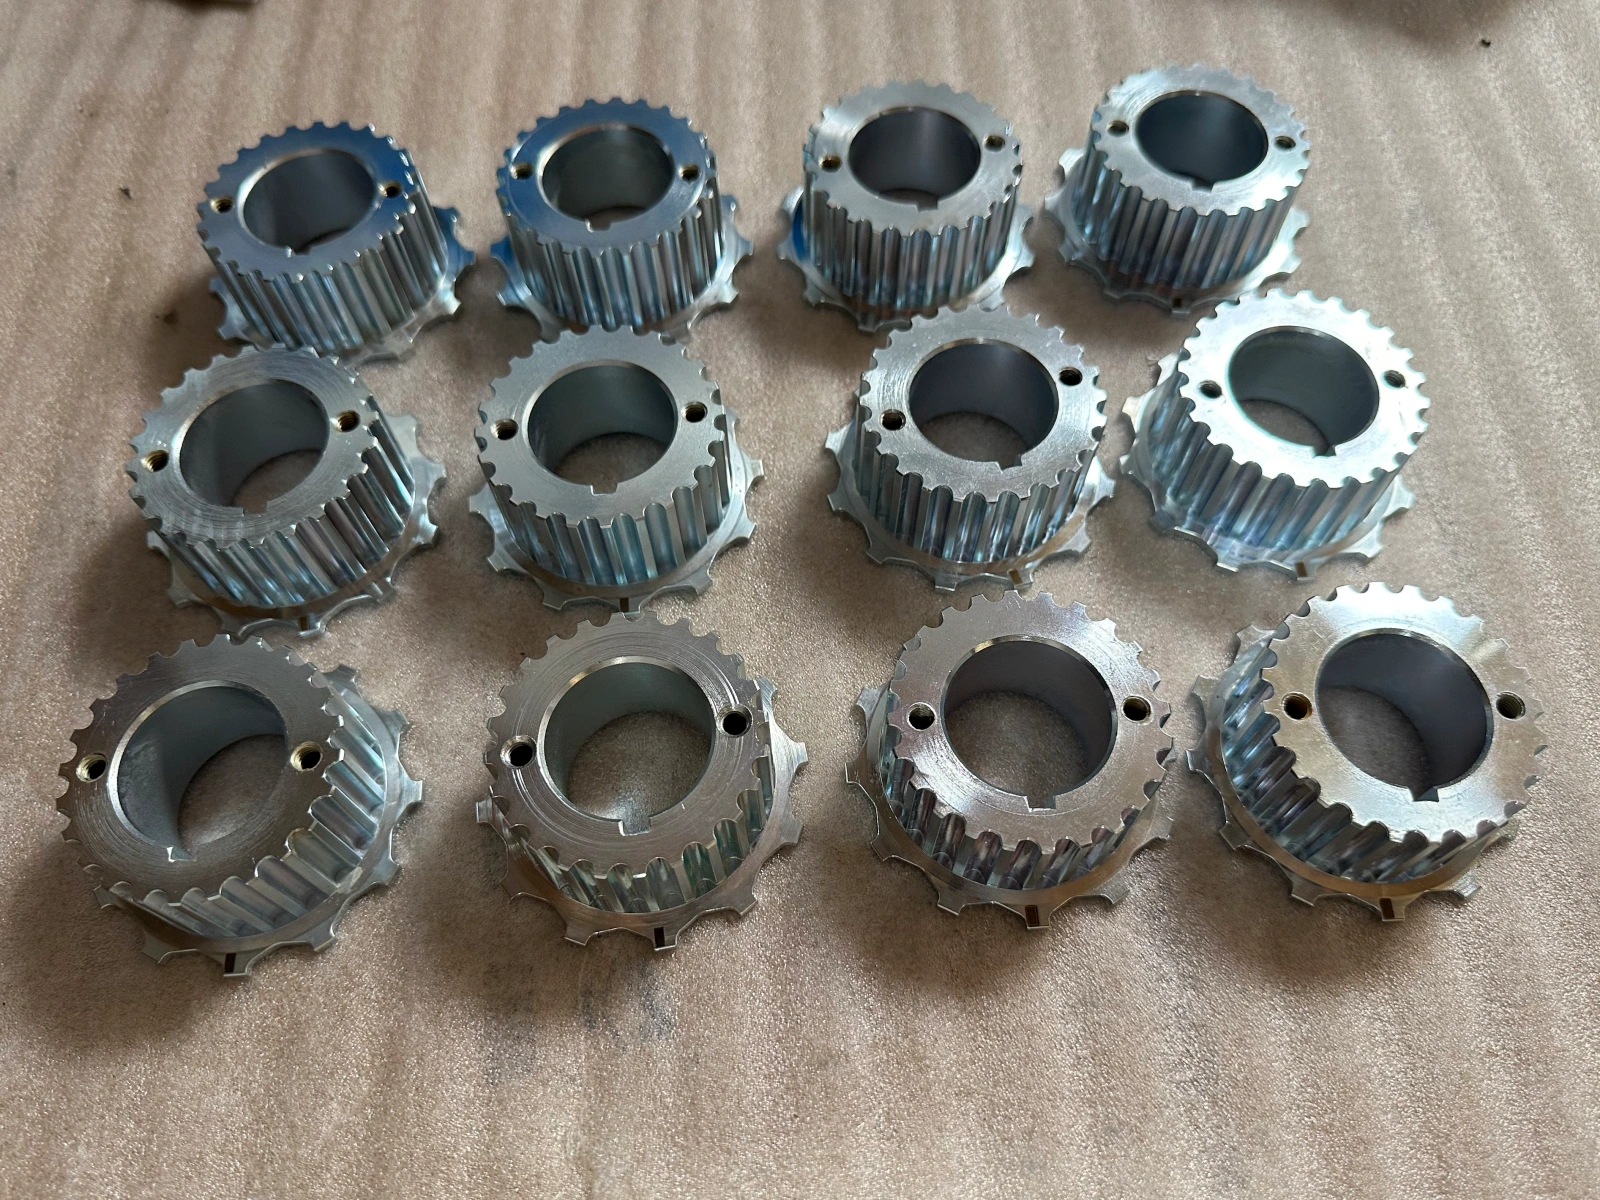
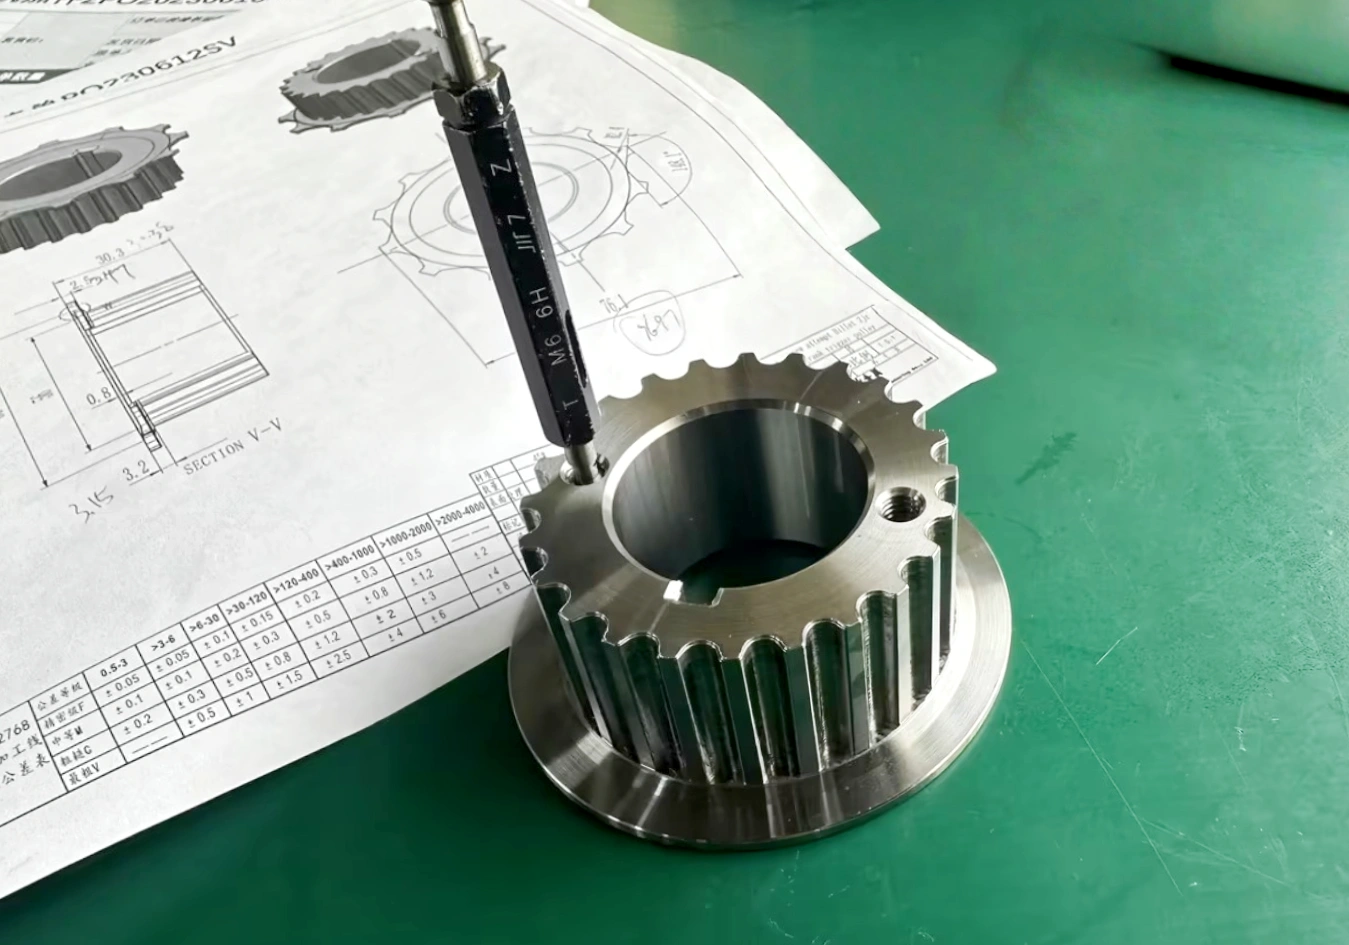
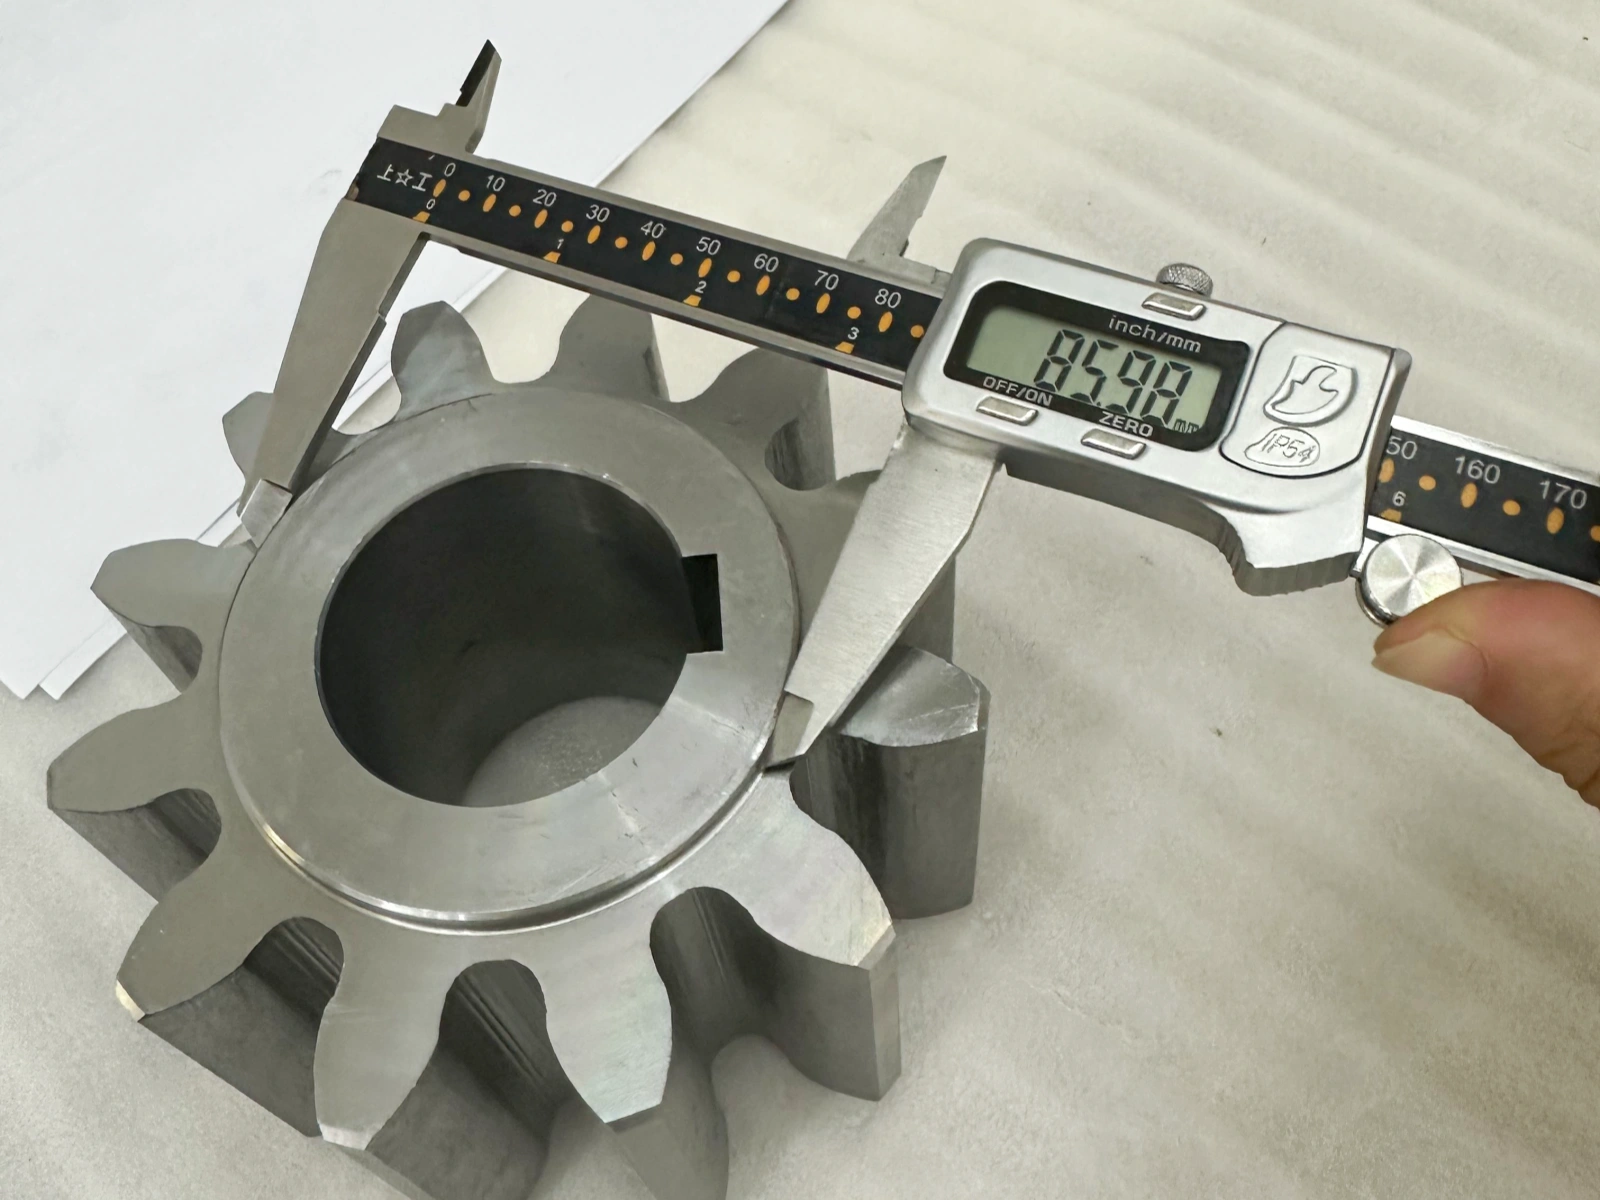

A part may need an additional process for gear teeth, conductive-material profiles, finished holes or internal threads. The process can be a main operation or follow milling or turning. Share the complete drawing so access, sequence and relationships between features can be reviewed.
Wire EDM requires an electrically conductive workpiece and is used for through-profiles along the wire path. Provide the material grade, thickness, contour and tolerances. Internal cutouts need a wire-entry route, and internal corners have finite radii. Blind pockets require a different approach.
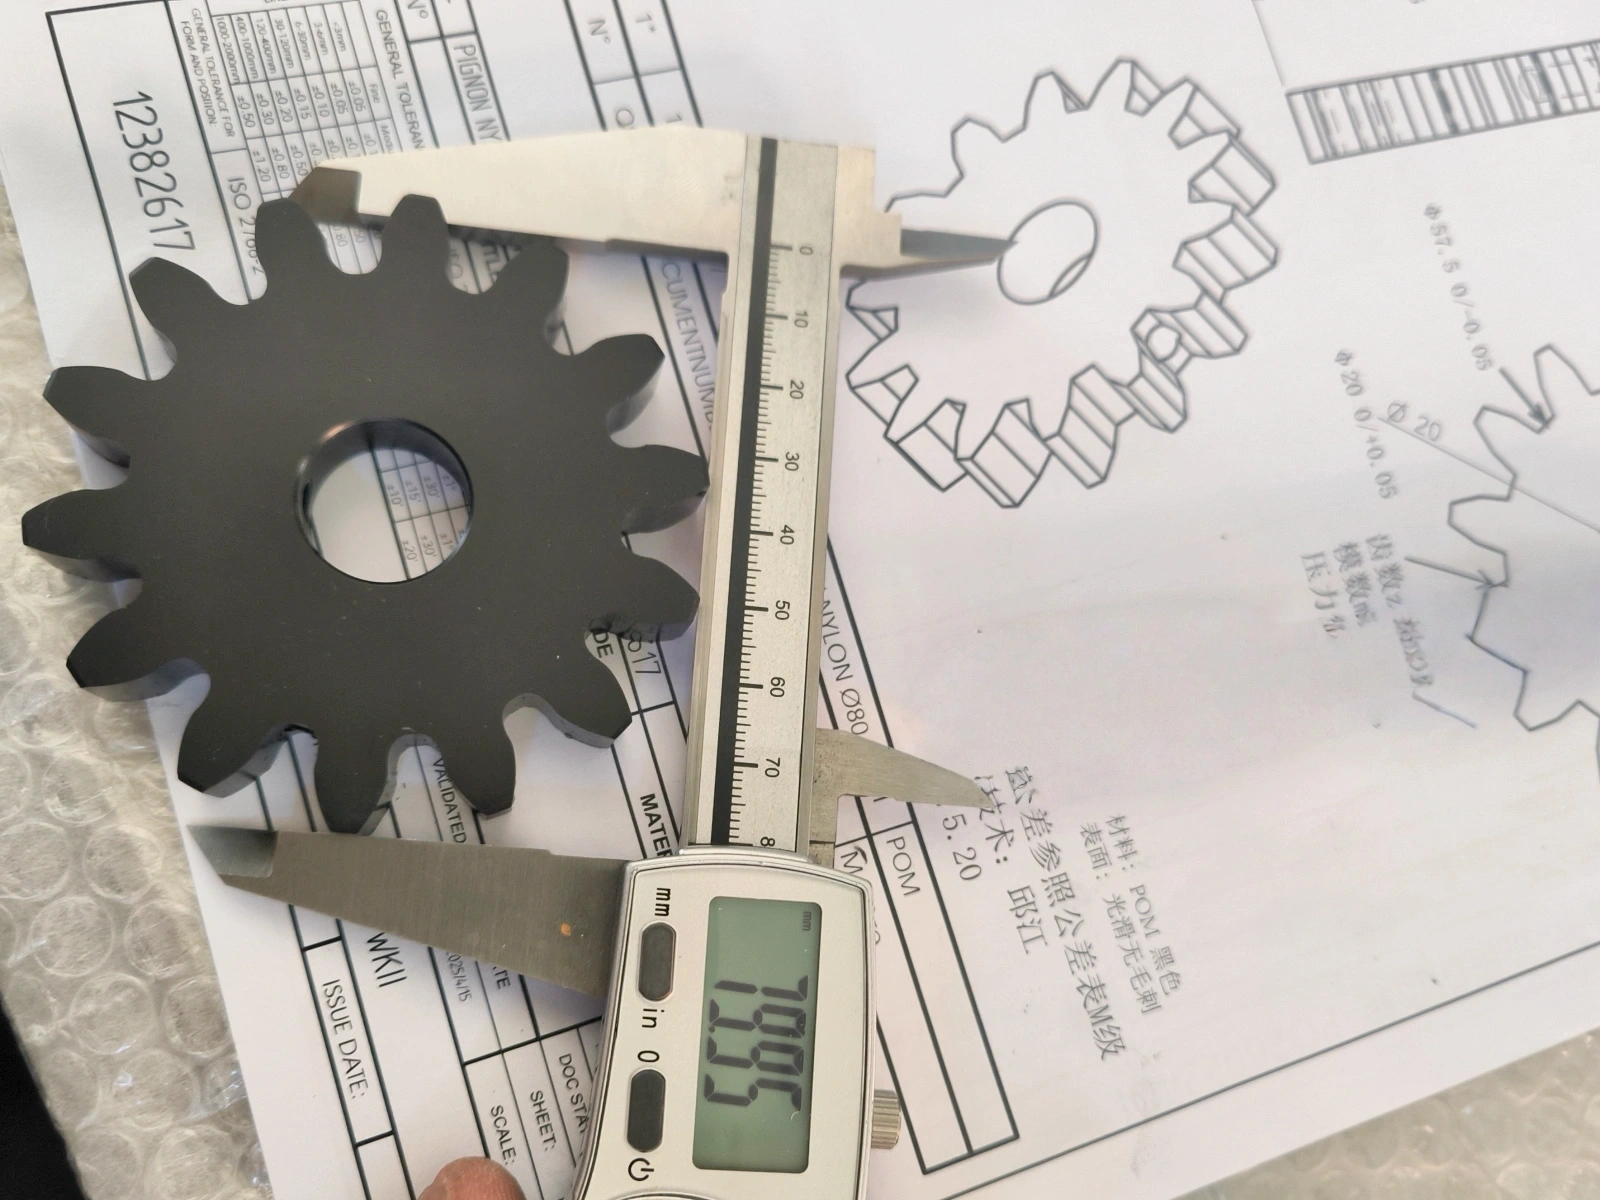
Provide the gear type, module or diametral pitch, tooth count, pressure angle and blank drawing. Helical gears also need helix angle and hand. Include material, heat treatment, accuracy standard and grade, together with inspection requirements. Tooling and clearance are confirmed before accepting the process.
No. External spur and helical gears can be reviewed for hobbing, subject to geometry and tooling. Internal gears, restricted shoulders and other tooth forms may require a different process. Do not assume that splines, worm-related components or post-hardening finishing are included without separate confirmation.
For drilling, provide finished diameter, depth, location and datums. For tapping, specify the thread standard, size, pitch, class where required and usable thread depth. Identify blind features, intersecting holes and access restrictions. State whether requirements apply before or after finishing.
Yes. Provide the complete part drawing and identify which operations are already finished. Datum preparation, remaining stock, heat treatment and access affect the sequence. The project review defines responsibilities and whether separate setups or processes are needed to meet the final specification.
Inspection follows the drawing and agreed acceptance criteria. Checks may cover EDM profiles, specified gear characteristics, hole dimensions and threads. Methods, sampling and reporting depend on the feature. Special gear measurements or surface-integrity testing must be identified and agreed before production.
Send the current drawing, model where available, material condition, quantity and target date. Add process-specific details such as EDM thickness and contour, gear specifications, hole requirements or thread details. Include inspection needs and previous operations. Pricing and lead time are confirmed after technical review.

This website uses cookies to provide you with a personalized browsing experience and analyze website traffic. By clicking "Accept", you agree to our use of cookies.
 Global